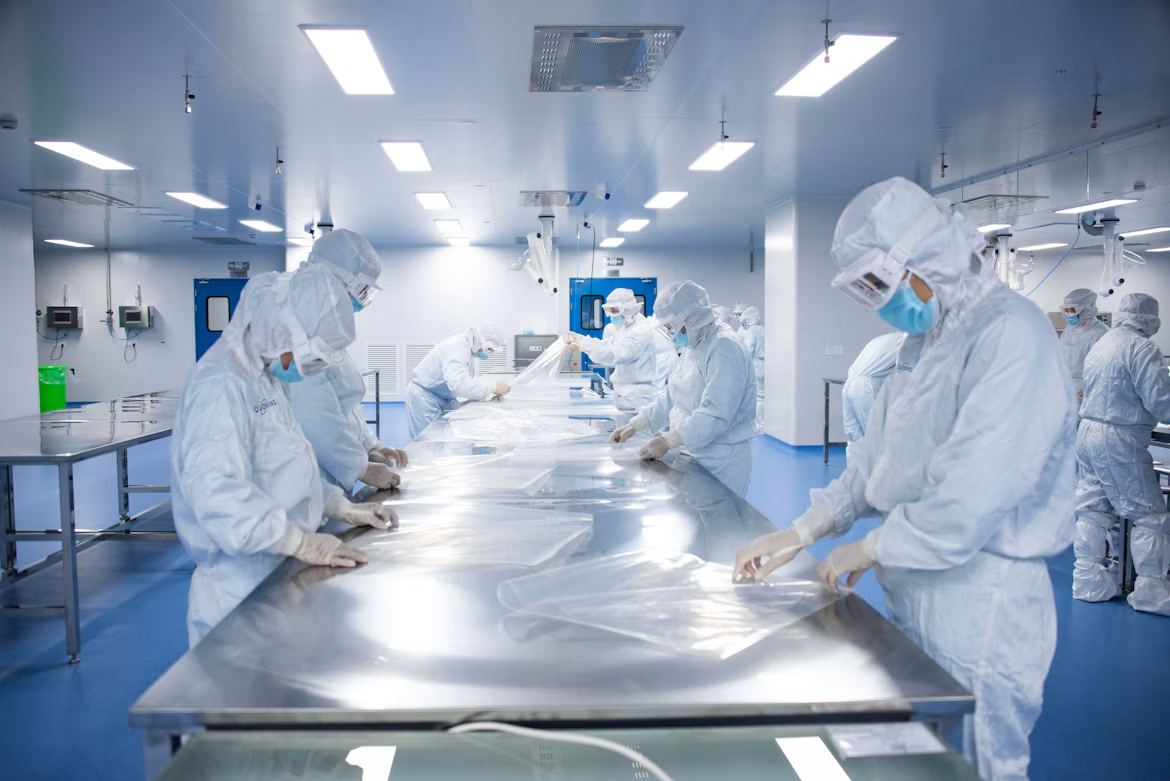
Aseptic manufacturing lines can lose time, product and capacity through small process weaknesses that remain invisible during routine production. A connection that takes too long to clean, an unstable filling rate or a poorly documented changeover may seem manageable in isolation.
Across hundreds of batches, however, these issues can reduce output and raise contamination risk. Manufacturers can address them by examining the full fluid path, measuring delays at each stage and selecting equipment suited to the formulation.
Hidden Downtime in Traditional Plants
Planned cleaning and sterilization schedules often conceal the true amount of unavailable production time. Operators may also wait for equipment to cool, test rinse samples, investigate alarms or repeat cleaning cycles. Common drivers of manufacturing downtime include maintenance gaps and process conditions that gradually reduce equipment performance.
Track the line from the final filled unit of one batch to the first acceptable unit of the next. Record cleaning, assembly, testing and approval as separate activities. A six-hour changeover may contain only two hours of required processing and four hours of waiting or repeated work. Looking at how manufacturers use production data to identify downtime and equipment issues can also help teams spot recurring losses that are easy to miss during routine operations.
Cross-Contamination Hazards
Product residue can remain in valves, transfer lines and other hard-to-reach areas even after a validated cleaning cycle. Small particles, degraded seals and improperly handled connectors introduce further risk. Similar hidden contamination sources can also contribute to equipment wear and unexpected stoppages.
Map every product-contact surface and review where operators must open, reconnect or manually clean the fluid path. For sensitive peptide formulations, closed assemblies can reduce the number of interventions required between formulation and filling. Manufacturers and CDMOs evaluating GLP-1 fill-finish solutions can consider customizable single-use fluid handling assemblies designed around sterility, viscosity and product yield requirements. Supplier qualification, incoming inspection and clear operator training should support any equipment change.
Upgrading High-Viscosity Filling Lines
High-viscosity formulations place different demands on tubing, pumps, connectors and filling needles. If the fluid path creates too much resistance, the line may deliver inconsistent volumes, run below its intended speed or expose the product to unnecessary stress. Temperature changes can further alter flow behavior during a batch.
Test the complete assembly with a representative fluid under expected operating conditions. Measure fill accuracy at startup, normal speed and near the end of the batch. Teams should also review tubing dimensions, pressure limits and hold-up volume before approving a configuration. For example, a line that meets its target at room temperature may drift after several hours if the formulation cools. Engineering trials can expose that weakness before commercial production begins.
Quantifying Return on Single-Use Gear
A financial assessment should include more than the purchase price of each assembly. Compare labor, water, cleaning agents, quality-control testing, sterilization time and lost production hours under the current process. Include the cost of discarded product left in tanks or transfer lines as well.
Calculate the value per batch first. If a disposable fluid path removes four hours of changeover time and the line contributes $8,000 per operating hour, the recovered capacity has a potential value of $32,000 before other savings. Then subtract assembly costs, disposal expenses, validation work and staff training. Run the calculation across low, expected and high production volumes so decision-makers can see where the investment becomes economical.
The strongest upgrade plan starts with one clearly defined fluid path and a measured baseline. A pilot on a difficult viscous formulation can reveal changes in fill accuracy, changeover time and recoverable product before the plant commits to a wider conversion.